
Stamping parts for medical devices once cost one of our clients a full production quarter. The parts measured fine. The paperwork did not. Our team learned that lesson the hard way.
Stamping parts for medical devices must meet biocompatibility standards under ISO 10993, comply with ISO 13485 and FDA 21 CFR Part 820, hold micron-level tolerances, use certified medical-grade materials, provide full lot traceability, pass validated cleaning and deburring, and withstand repeated sterilization.
That is a long list. But each requirement exists for a clear reason. Let me walk you through what buyers must check, step by step, before approving any medical stamping supplier.
What quality standards must I verify before sourcing stamping parts for medical devices?
A few years back, a U.S. purchasing manager sent our Singapore office a bracket drawing that looked simple. Then he added two words: "medical use." Everything about the sourcing plan changed that day.
Before sourcing stamping parts for medical devices, verify ISO 13485 certification, FDA 21 CFR Part 820 compliance, ISO 10993 biocompatibility test data, documented tolerances of ±0.01mm or tighter on critical features, burr-free surface finish standards, and validated process controls with statistical capability evidence.

Medical stamping is different from general industrial stamping. A part can be dimensionally perfect and still fail. Why? Because in medical work, a "good part" must be both technically correct and compliance-ready. The proof matters as much as the part.
The core standards you cannot skip
Here is a summary of the standards buyers should confirm first:
| Standard | What It Covers | Why It Matters for Stamped Parts |
|---|---|---|
| ISO 13485 1 | Quality management system for medical devices | Baseline requirement for any medical supplier |
| FDA 21 CFR Part 820 2 | U.S. quality system regulation | Mandatory for parts entering U.S. devices |
| EU MDR 2017/745 3 | European medical device regulation | Required for EU-market devices |
| ISO 10993 4 | Biocompatibility testing | Confirms material safety for tissue or fluid contact |
| MDSAP | Single audit for multiple markets | Efficient proof across regulatory regions |
Tolerances and surface quality
Medical stamping tolerances are often measured in microns. Critical features may need to hold below 0.01 mm, or around ±0.0005 inches. Small deviations can break assembly fit, sealing, or motion in a device.
Surface requirements are equally strict. A common benchmark is Ra ≤ 0.8 µm for non-implantable contact surfaces and Ra ≤ 0.4 µm for implantable ones. Burrs and rough edges are not cosmetic issues. They can trap bacteria, shed particles, and irritate tissue.
For high-risk Class III components, expect statistical process control expectations too. A minimum Cpk of 1.33 is a typical benchmark for demonstrating long-term process capability. In our sourcing audits across Vietnam and other Asian regions, we check whether a shop actually runs SPC charts on the press line, not just at final inspection.
How do I ensure my supplier meets FDA and ISO 13485 compliance for medical stamping parts?
There is a trade-off we weigh on every medical project: certified suppliers cost more, but uncertified ones cost far more when an audit fails. Our audit team in Vietnam has seen both outcomes up close.
Verify the supplier's current ISO 13485 certificate through the registrar, review recent audit reports, confirm FDA registration where applicable, request IQ/OQ/PQ validation records, inspect document control and CAPA systems on-site, and run a first-article inspection before releasing any production order.

Certificates alone do not prove compliance. I have walked factory floors where a framed ISO 13485 certificate hung on the wall while the press operators used uncontrolled drawing revisions. That gap is exactly what an FDA auditor will find later. So verification must go deeper than paperwork.
A practical verification sequence
Follow this order. It saves time and exposes weak suppliers early.
- Check the certificate itself. Confirm the scope covers stamping of medical components, not just general metalwork. Verify the registrar and expiry date.
- Request the latest audit findings. Ask for the most recent surveillance audit summary and any open nonconformities.
- Review process validation. IQ/OQ/PQ validation is expected for processes producing medical components. That includes stamping, cleaning, deburring, passivation, and packaging where risk requires it.
- Audit on-site or through a local partner. Look at document control, training records, calibration logs, and the CAPA system. A supplier who cannot show a closed CAPA loop cannot survive a regulator's visit.
- Run a first-article inspection with full documentation. Match every dimension, material cert, and surface spec against the drawing before approving volume production.
Why the process matters more than the final check
In medical manufacturing, inspecting the finished part is not enough. The process itself must be proven capable and repeatable. Think of it as a simple formula: validated process plus documented controls equals acceptable medical production. When we manage PPAP submissions for U.S. clients, we treat the validation package as the deliverable, not just the parts in the box. One important nuance: the stamping supplier is usually not regulated the same way as the finished device. Instead, the device manufacturer qualifies the supplier through its own quality system. That is why your supplier audit carries so much weight.
What material certifications should I request for medical-grade stamping components?
A buyer once asked me why we rejected a coil of 316 stainless that his previous vendor had used for years. The mill test report showed sulfur levels fine for industrial use but risky for his fluid-contact application. Paper caught what eyes could not.
Request the mill test report with full chemical composition, a certificate of conformity to the exact material grade such as 316L stainless or titanium, ISO 10993 biocompatibility test data for the intended contact type, heat lot numbers for traceability, and certification of any plating or passivation processes.

Material selection for medical stamping goes far beyond strength. The metal must survive the device's whole life. That includes forming stress, cleaning chemicals, body fluids, and repeated sterilization cycles. A material that performs well in industrial stamping can fail in medical use if it degrades under autoclave heat or reacts with cleaning agents.
Common medical stamping materials and their roles
| Material | Typical Use | Key Certification Points |
|---|---|---|
| 316L stainless steel | Surgical instruments, brackets, clips | Low-carbon grade cert, corrosion resistance, passivation records |
| Titanium 5 | Implants, structural components | Grade verification, ISO 10993 data, fatigue properties |
| Nitinol (nickel-titanium) | Stents, flexible components | Transformation temperature cert, nickel-release data |
| 17-7 PH stainless | Springs, retaining clips | Heat treatment records, hardness certification |
Match the material to sterilization and environment
Sterilization method 6 drives material choice. Steam autoclaving, EtO gas, gamma radiation, and e-beam each stress materials differently. Ask your supplier to confirm the material's dimensional stability and corrosion behavior under your specific sterilization method. Many modern devices must survive multiple methods, which raises the bar further.
Two more checks matter for specific applications. First, if the assembly joins dissimilar stamped metals, request a galvanic corrosion 7 risk assessment. Body fluids act as an electrolyte and can drive electrochemical degradation between mismatched metals. Second, if the component will sit near or inside an MRI environment, confirm the material is non-ferromagnetic to avoid imaging artifacts and patient safety risks.
One last distinction our engineers stress with clients: material biocompatibility and surface biocompatibility are not the same thing. The same base alloy can behave differently depending on forming, cleaning, passivation, plating, or contamination control. So the certification package must cover the finished surface, not just the raw coil.
How can I confirm my stamping partner has the right cleanroom and traceability processes for medical parts?
Early in our custom-parts business, we assumed a clean shop floor meant clean parts. Then a client's incoming inspection found oil residue on components that had measured perfectly. That shipment taught our whole team what "cleanliness" actually means in medical work.
Confirm your partner documents end-to-end traceability from raw material heat lot through stamping batch, heat treatment, and final inspection, retains records for over 10 years, uses validated cleaning processes, and cleans or packs higher-risk parts in ISO Class 7 or 8 cleanroom environments.

Traceability is mandatory in medical manufacturing, not optional. When a device fails in the field, the manufacturer must trace every component back through its full history. Recalls, complaint investigations, supplier qualification, and regulatory audits all depend on that chain of records. A stamping partner who cannot produce lot-level documentation on demand is a liability, no matter how good the parts look.
What a complete traceability chain looks like
| Stage | Required Record | Purpose |
|---|---|---|
| Raw material | Mill test report, heat lot number | Links every part to certified material |
| Stamping | Batch record, press parameters, tool ID | Isolates affected lots if issues arise |
| Post-processing | Heat treat, deburr, passivation records | Proves validated secondary operations |
| Inspection | Dimensional reports, surface checks | Documents conformity per lot |
| Packaging | Controlled packaging records, lot labels | Prevents mix-ups and contamination |
Records may need to be retained for more than ten years. Ask your supplier directly how long they keep batch files and how fast they can retrieve them.
Cleanliness is a separate discipline
A perfectly stamped component can still be rejected if it carries oils, particles, or residue. Contamination threatens sterility and can interfere with sterilization effectiveness, because residues shield microbes from the sterilant. For implantable or high-risk parts, cleaning and packing in ISO Class 7 or 8 cleanrooms is increasingly the expectation, not a premium option.
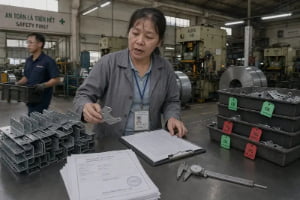
When our team audits stamping shops across Asia, we check three things in this area. First, is the cleaning process validated, or just assumed? Deburring and cleaning must be validated like any other medical process. Second, does packaging protect parts from particulate contamination during door-to-door transit? Third, does the shop control what touches the part after cleaning, including gloves, trays, and bags? Those small details decide whether parts arrive compliance-ready or become another rework story.
Conclusion
Medical stamping demands precision plus proof: biocompatibility, validated processes, traceability, and cleanliness. Our team helps buyers verify all of it before parts ship. Choose partners who deliver both.
Footnotes
1. Official ISO standard page defines medical device quality management system requirements referenced throughout. ↩︎
2. FDA’s official quality system regulation page explains the compliance requirement mentioned repeatedly. ↩︎
3. Wikipedia background on the European medical device regulation referenced in the standards table. ↩︎
4. Official ISO page for biocompatibility testing standard cited as core requirement in the article. ↩︎
5. Background reference on titanium properties relevant to implant-grade stamped components discussed.
 English
 Español de México
 Deutsch
 Français
 Русский
 العربية
Leave a Comment
Your email address will not be published. Required fields are marked *