
Quality inspections for stamping parts decide whether your shipment assembles cleanly or gets rejected ISO 2859-1 1. I have watched buyers lose weeks over one skipped check on our sourcing projects.
Before leaving the factory, stamping parts must pass incoming material verification, first article inspection, in-process checks, and final outgoing inspection covering dimensions, burrs, cracks, surface defects, functional fit, hardness or coating tests, packaging, and full documentation review including material certificates and traceability records.
That sounds like a lot. It is. But each check exists because a specific defect slips through without it coordinate measuring machine 2. Let me walk you through the whole chain, step by step.
How Do I Know If My Stamping Supplier's Final Inspection Process Is Reliable?
A purchasing manager once asked me to audit a stamping plant in Vietnam after two straight rejected lots ISO 2859-1 sampling 3. The gap we found was simple: no defined final inspection gate at all.
A reliable final inspection process has a written outgoing quality control (OQC) procedure, defined AQL sampling plans, calibrated measurement tools, dedicated inspectors independent of production, documented inspection records for every lot, and clear hold-and-release rules for non-conforming stamping parts.

When our team audits stamping suppliers across Vietnam, Taiwan, and India, we do not start with the parts. We start with the paperwork and the people. A factory can show you a beautiful sample. It cannot fake a two-year inspection record trail.
What We Look for During a QC Audit
First, we check independence. The final inspector should not report to the production manager. If the same person who runs the press also signs off the lot, defects get "negotiated" instead of caught.
Second, we check the sampling plan. A serious supplier follows ANSI/ASQ Z1.4 4 or ISO 2859-1 sampling. Critical dimensions get a tighter AQL than cosmetic features. Ask your supplier what AQL they apply to your part. If they cannot answer, that is a red flag.
Third, we verify calibration. Calipers, micrometers, and gauges must carry valid calibration labels. Expired calibration means every measurement is questionable.
| Reliability Signal | What Good Looks Like | Red Flag |
|---|---|---|
| OQC procedure | Written, version-controlled document | Verbal "we always check" |
| Sampling plan | AQL defined per defect class | Random spot checks |
| Inspector independence | Separate QC department | Operator self-inspection only |
| Tool calibration | Current labels, calibration log | No labels, no records |
| Non-conformance handling | Hold area, documented disposition | Rework mixed with good stock |
| Records | Lot-by-lot inspection reports | Reports created on request |
Finally, ask for the last three lot inspection reports for a similar part. Real records show dates, measured values, inspector names, and occasional rejections. A file with zero rejections ever is usually a file written yesterday.
What In-Process Quality Checks Should Happen Before Stamping Parts Reach Final Inspection?
There is a trade-off we weigh on every stamping project: more in-process checks slow the press, but fewer checks push all the risk to the final gate. Final inspection alone cannot save a bad run.
Before final inspection, stamping parts should pass incoming material verification, first article inspection on every new setup, and in-process checks at set intervals covering critical dimensions, burr height, crack detection, tool wear monitoring, and surface condition, so defects are stopped early rather than shipped.

Think of quality as a chain with four links. If the first three links are weak, the final inspector becomes a defect sorter instead of a gatekeeper. Sorting is expensive and unreliable. Prevention is cheaper.
The Four-Stage Inspection Flow
- Incoming material inspection. The coil or sheet gets checked before it touches the press. Inspectors review the mill test certificate, measure thickness and flatness, and look for rust, scratches, and contamination. Wrong material grade here ruins the entire lot later.
- First article inspection (FAI). The first parts off a new die or new setup get measured against every drawing dimension. Production does not start until the first article passes. On our projects, we require FAI sign-off after every die change, not just the first order.
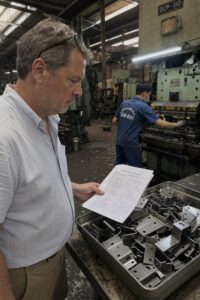
- In-process inspection. Operators and patrol inspectors check parts at fixed intervals, often every hour or every set number of strokes. They watch critical dimensions, burr formation, and surface defects. They also monitor the die, because tool wear is the number one cause of drifting dimensions and growing burrs.
- Final outgoing inspection. The last gate. It confirms what the earlier stages should have already guaranteed.
Why Tool Wear Monitoring Matters
Burrs do not appear suddenly. They grow as the punch and die edges wear. A good factory tracks burr height over the run and pulls the die for sharpening before parts go out of spec. On spring clips and brackets like the ones we source, an oversized burr can cut an assembler's hand or block a mating surface. Catching it mid-run costs minutes. Catching it in your warehouse costs a return shipment.
Which Measurement Tools and Methods Are Essential for Verifying Stamping Part Accuracy?
Early in one bracket project, our engineers found that a supplier was checking a bend angle with a plastic protractor. The drawing called for ±0.5 degrees. That mismatch between tool and tolerance explained every rejected lot.
Essential tools for verifying stamping part accuracy include calipers and micrometers for basic dimensions, height gauges for flange positions, go/no-go gauges and check fixtures for fast fit verification, CMMs or 2.5D vision systems for tight tolerances, and hardness testers for material properties.

The right tool depends on the tolerance and the feature. Using a caliper on a ±0.02 mm dimension is guesswork. Using a CMM on a ±0.5 mm dimension is wasted money. Matching the instrument to the requirement is a core skill we test during supplier audits.
Matching Tools to Features
| Feature Type | Typical Tolerance | Recommended Tool |
|---|---|---|
| Overall length/width | ±0.1 to ±0.3 mm | Digital caliper |
| Material thickness | ±0.02 to ±0.05 mm | Micrometer |
| Hole diameter | ±0.05 mm | Pin gauge / go-no-go plug |
| Hole position | ±0.05 to ±0.1 mm | CMM or 2.5D vision system |
| Bend angle | ±0.5 to ±1 degree | Angle gauge, profile projector |
| Flange height | ±0.1 mm | Height gauge, check fixture |
| Overall fit | Assembly envelope | Dedicated check fixture |
| Hardness/springback | Per material spec | Hardness tester |
Fixtures Versus Metrology
Check fixtures and go/no-go gauges answer one question fast: does the part fit? They are perfect for 100% or high-frequency checks on the line. But they give a pass/fail result, not a number.
CMMs and vision systems give actual measured values. Those numbers feed SPC charts and Cpk calculations process capability 5, which tell you whether the process is stable or drifting toward the tolerance edge. For precision parts, many customers require Cpk of 1.33 or higher on critical dimensions. You cannot calculate Cpk from a go/no-go gauge.
For formed parts like Z-shaped spring clips, springback adds another layer. The metal relaxes after forming. Good factories measure critical angles after a stabilization period, not straight off the press, so the recorded dimension matches what you receive.
How Can I Confirm My Stamping Parts Meet PPAP and Documentation Requirements Before Shipment?
Greg, a purchasing manager we work with in the US, once told me his previous supplier shipped conforming parts with useless paperwork, and his end customer rejected the whole delivery anyway. Documentation is not decoration. It is part of the product.
Confirm PPAP compliance by requiring a submitted PPAP package before first shipment, including dimensional results, material certificates, process flow diagram, control plan, PFMEA, and capability studies, then verify every production lot ships with an inspection report, certificate of conformity, and traceable lot codes.

On our custom parts projects, PPAP is the bridge between "the sample was fine" and "every future lot will be fine." It forces the supplier to document how the part is made, how it is controlled, and how capable the process really is. When we manage PPAP for clients, we review the package before it ever reaches their inbox.
The Core PPAP Elements for Stamping Parts
| PPAP Element | What It Proves |
|---|---|
| Dimensional results | Every drawing dimension was measured on real parts |
| Material certification | Correct grade and thickness were used |
| Process flow diagram | The production route is defined and repeatable |
| Control plan | Each critical characteristic has a defined check method and frequency |
| PFMEA 6 | Failure risks were analyzed and mitigated |
| Capability studies (Cpk/Ppk) | Critical dimensions are statistically stable |
| Master sample | A physical reference exists for future comparison |
What to Check on Every Shipment After PPAP
PPAP approval is the starting line, not the finish line. For each production lot, your supplier should provide a final inspection report with measured values, a certificate of conformity 7, and lot traceability. Traceability means the lot code on the label links back to the material coil, the die, the press, and the inspection records. If a defect surfaces six months later, that code tells you exactly which lots are at risk and which are safe.
Packaging verification belongs here too. Correct quantity, proper separators, rust-preventive protection, and accurate labels are all part of final release. A perfect part that arrives corroded is still a rejected part.
Conclusion
Skipped inspections turn into rejected shipments, rework, and missed launches. A full chain of checks, from incoming material to PPAP-backed final release, is the fix.
Quality inspections for stamping parts are not one test at the end. They are a system: material verification, first article approval, in-process control, calibrated measurement, and a documented final gate with traceability. When we manage stamping projects for US and European clients, we hold suppliers to every link in that chain, because getting it right the first time is always cheaper than sorting it out after the container lands. If you want a second set of eyes on your supplier's QC process, that is exactly the work our team does every day.
Footnotes
1. Official ISO standard page for the sampling procedure mentioned in the article. ↩︎
2. Background explanation of CMM technology used for tight tolerance verification. ↩︎
3. ISO standard defines acceptance sampling procedures referenced for stamping part QC plans. ↩︎
4. Explains acceptance sampling standard referenced for AQL sampling plans. ↩︎
5. Explains Cpk/Ppk statistical concept used for capability studies in the article. ↩︎
6. Wikipedia overview of failure mode analysis methodology referenced in PPAP elements. ↩︎
7. ISO reference for conformity certification standards mentioned in shipment documentation. ↩︎
 English
 Español de México
 Deutsch
 Français
 Русский
 العربية
Leave a Comment
Your email address will not be published. Required fields are marked *