
Judging a supplier’s [composite stamping capability](https://dewintech.com/blog/how-evaluate-supplier-compound-stamping-capability-sourcing-parts/) from a quote sheet is risky. I have audited stamping plants across Vietnam and China where the brochure and the shop floor told two very different stories.
Evaluate a supplier’s composite stamping capability by verifying press and tooling fit for your part, auditing the quality system beyond certificates, demanding PPAP, FAI, and SPC evidence, assessing engineering and DFM support, and confirming a documented on-time delivery record through a site audit.
That is the short answer. Now let me walk you through each step, using what our audit team actually checks before we award a stamping program on behalf of our U.S. clients.
What Should I Check in a Supplier's Stamping Equipment and Tooling Before Placing an Order?
A few years back, our Vietnam team visited a stamper with impressive press tonnage on paper. The dies for progressive work, however, were outsourced with no maintenance log. We walked away.
Check that press type, tonnage, stroke, and bed size match your part geometry, material, and volume. Then verify who designs, builds, and maintains the dies. In-house progressive and transfer die capability, with documented maintenance and die-life tracking, signals a lower-risk stamping partner.

Equipment and tooling are the foundation of composite stamping capability. But headline numbers mislead. A 400-ton press means nothing if the bed size cannot hold your progressive die, or if the press type cannot hold tolerance on your material. When we qualify stampers for multi-flange brackets and spring clips, we start with the part, not the press list.
Match the Press to Your Part, Not the Brochure
Ask the supplier to map your specific part to a specific press. Which machine will run it? What is the planned strokes-per-minute rate? Can they sustain dimensional control over a long run on your material thickness? For advanced high-strength steel or complex geometries, ask about servo press capability 1. Servo presses give better control of forming speed and springback, which matters on tight-tolerance bent parts.
Dig Into Tooling Ownership
Tooling is where programs quietly fail. In our experience managing contract manufacturing 2 for U.S. buyers, outsourced tooling is not automatically bad, but it demands stronger governance. Ask these questions directly:
- Who owns the die, and is that stated in the contract?
- Who performs die maintenance, and on what schedule?
- How are die wear, corrections, and engineering revisions managed?
- What is the tooling repair turnaround time when a die cracks mid-run?
| Checkpoint | What Good Looks Like | Red Flag |
|---|---|---|
| Press fit | Specific press assigned to your part with tonnage margin | Vague "we have many presses" answers |
| Die design | In-house design and tryout, simulation used | Fully outsourced with no oversight records |
| Die maintenance | Logged preventive maintenance, die-life counters | Maintenance done "when problems appear" |
| Repair turnaround | Tool room on-site, hours-to-days response | Weeks of downtime waiting on external shops |
| Revision control | Documented ECN process tied to die changes | Operators adjusting dies informally |
A supplier who can show you die maintenance logs and die-life data without hesitation is usually a supplier who controls their process.
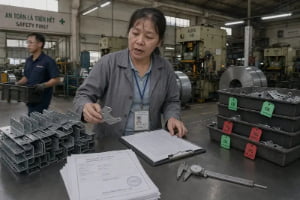
How Can I Verify a Supplier's Quality Control Process to Avoid Non-Conforming Parts?
One buyer we work with, a purchasing manager in the U.S., once received a full container of brackets with an overlooked slot tolerance. That single miss cost him weeks. It shaped how we now audit QC.
Verify quality control by requesting sample PPAP or FAI packages from comparable programs, reviewing live SPC data on critical dimensions with Cpk of 1.33 or higher, inspecting CMM and gauge calibration records, and confirming material traceability from coil to finished shipment. Certificates alone prove nothing.

Certifications like ISO 9001 3 or IATF 16949 are a baseline filter, not proof. I have stood in certified plants where the control plan on the wall did not match what operators actually did. So our final inspection team treats certificates as a gate, then verifies actual behavior.
Demand Documented Compliance and Demonstrated Capability
There is a difference between documented compliance and demonstrated process capability. You need both. Documented compliance means control plans, inspection instructions, and corrective action procedures exist and are followed. Demonstrated capability means the data shows the process holds tolerance run after run.
Ask for a Level 3 PPAP 4 package from a prior, comparable program. Look at completeness and turnaround speed. Then ask for SPC charts 5 on critical dimensions. A Cpk of 1.33 or higher is the standard threshold worth insisting on for critical features. If the supplier can only show retrospective summaries, ask to observe live SPC during an active production run. That single request separates real process control from paperwork theater.
Check Metrology and Traceability
| QC Element | What to Request | Why It Matters |
|---|---|---|
| PPAP / FAI | Sample package from a similar part | Proves real-world documentation discipline |
| SPC / Cpk 6 | Recent capability data, Cpk ≥ 1.33 on critical dims | Proves repeatability, not just intent |
| CMM / gauges | Calibration certificates and schedules | Uncalibrated tools make all data worthless |
| Traceability | Coil-to-shipment lot linkage, mill certs on file | Enables fast containment of any defect |
| In-process checks | Frequency, burr control, plating and packaging plans | Catches drift before it becomes scrap |
Also confirm how the supplier handles drawing revisions. In our experience, revision-control failures cause more non-conforming shipments than machine failures do.
What Questions Should I Ask to Assess a Supplier's Engineering and Co-Development Capabilities?
When we co-develop stamped clips with clients, the best moments happen before quotation. A good stamper once flagged springback risk on a Z-fold profile our client had drawn. That early call saved a die rework.
Ask whether the supplier runs DFM reviews and feasibility studies before quoting, uses forming simulation to predict springback and thinning, supports prototyping and material selection, and communicates technical risks honestly. Strong engineering support reduces tooling iterations, scrap, and downstream program risk.

Engineering support is the most underrated part of composite stamping capability. A supplier who simply quotes your drawing is a vendor. A supplier who challenges your drawing constructively is a partner. Our project management team has learned to test this early, because weak engineering shows up later as tolerance disputes and blame-shifting.
The Questions That Reveal Engineering Depth
Use this sequence in your RFQ discussions:
- Can you review our drawing and flag manufacturability risks before quoting?
- How do you manage springback on this material and bend geometry?
- Do you run forming simulation 7 or rely only on tryout iterations?
- What material grade or thickness alternatives would you suggest, and why?
- Can you produce prototypes or soft-tool samples before hard tooling?
- How do you handle engineering changes after tooling kickoff?
- Who is our single technical point of contact during development?
Listen for specifics. A capable engineering team answers with material grades, bend radii, and simulation outputs. A weak one answers with "no problem, we can do it." In our co-development work, "no problem" is often the biggest problem. It usually means critical drawing requirements were not actually read.
Judge the Communication, Not Just the Answers
Response speed and clarity during the RFQ stage predict behavior during production. If a supplier takes ten days to answer a feasibility question before you place an order, imagine the response time when a die cracks mid-program. We score suppliers on RFQ review discipline for exactly this reason: it is the cheapest early warning signal a buyer can get.
How Do I Confirm a Supplier's On-Time Delivery Track Record for Composite Stamping Projects?
Delivery delays are the single most common complaint we hear from U.S. purchasing managers switching to our sourcing service. Almost every delay traces back to something visible during the audit, if you know where to look.
Confirm on-time delivery by requesting the supplier's OTD data for the past twelve months, checking capacity utilization and staffing stability, reviewing die maintenance and repair turnaround records, verifying MES or ERP tracking of live orders, and calling references from clients with similar volumes.

On-time delivery is not luck. It is the output of capacity planning, tooling uptime, material availability, and honest scheduling. When our team audits a stamper's delivery reliability, we treat the supplier's claimed OTD percentage as a starting point, then verify the systems behind it.
Look at the Systems That Produce On-Time Delivery
A supplier can only ship on time consistently if certain foundations exist. Check each one:
| Delivery Driver | What to Verify | Warning Sign |
|---|---|---|
| OTD history | 12-month OTD data, ideally by customer | No data tracked, or "we are always on time" |
| Capacity | Current utilization and volume headroom | Presses running near 100% with no buffer |
| Tooling uptime | Die repair turnaround, spare die policy | Single die, external repair, no spares |
| Material supply | Coil stock policy, incoming inspection lead time | Material ordered only after PO receipt |
| Digital tracking | MES/ERP lot tracking, real-time order status | Production status kept in someone's notebook |
| Scalability | Ability to absorb rush orders and volume increases | Every rush order requires "special arrangement" |
Test Scalability, Not Just Launch Performance
Many suppliers deliver the first order on time and drift afterward. Sustained production over hundreds of thousands of cycles is a different test than launch. Ask how they handled their last rush order. Ask what happened the last time a die failed mid-run. Ask for scrap and yield rates on comparable jobs, since low waste signals mature process control and stable throughput. Then call a reference customer with similar volumes and ask one question: did shipments stay on time after month six? In our supplier audits, we also watch how planning meetings actually run, because a plant that plans daily rarely surprises you monthly.
Conclusion
Evaluating composite stamping capability means verifying press fit, tooling control, quality evidence, engineering depth, and delivery systems—then auditing the factory before award. Discipline beats price every time.
Footnotes
1. Provides technical background on servo press technology referenced for forming speed and springback control. ↩︎
2. Alibaba.com is a leading sourcing platform relevant to global contract manufacturing arrangements. ↩︎
3. Official ISO page explaining the quality management standard referenced as a supplier baseline. ↩︎
4. AIAG publishes the PPAP manual, the authoritative source for this documentation process. ↩︎
5. Background reference explaining statistical process control charts used to verify capability. ↩︎
6. Explains the process capability index metric cited as the quality threshold standard. ↩︎
7. Background concept on metal forming relevant to simulation used for springback prediction. ↩︎
 English
 Español de México
 Deutsch
 Français
 Русский
 العربية
Leave a Comment
Your email address will not be published. Required fields are marked *