
Comparing the overall strength of stamping parts suppliers is hard when every quote looks similar CAD/CAM capability 1. Our audit team learned this the expensive way — a low quote once cost a client three months of rework.
Compare stamping parts suppliers across five dimensions: quality certifications and process data (Cpk, FAI, SPC), engineering and tooling capability, production capacity, on-time delivery history, and total program cost. Score each supplier on a weighted matrix, then verify claims with documents and an on-site audit.
That is the short answer. Now let me walk you through how we actually do this in practice, section by section, so you can apply the same framework to your own sourcing decisions.
What Quality Control Standards Should I Expect from a Reliable Stamping Parts Supplier?
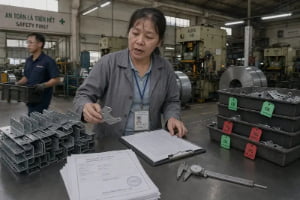
A few years back, our team audited a stamping plant in Vietnam that had a beautiful showroom but no calibration records for its CMM DFM report 2. That contrast taught us where to look first.
A reliable stamping parts supplier should hold ISO 9001 at minimum, plus IATF 16949 or AS9100 where relevant, and prove it with first-article inspection reports, SPC charts, Cpk data on critical dimensions, calibrated inspection equipment, and full material traceability from coil to finished part.

Certificates are the entry ticket, not the finish line. When we run supplier audits for U.S. clients, we treat the certificate as a claim and the shop-floor data as the evidence. A supplier can frame an ISO 9001 certificate 3 on the wall and still ship brackets with holes punched off-position. So we always ask for proof tied to a real part, ideally one similar in geometry and tolerance to yours.
The Documents That Actually Prove Quality
Here is the evidence package we request before any contract:
| Evidence | What It Proves | Red Flag If Missing |
|---|---|---|
| FAI / PPAP documentation | The supplier can validate a new part correctly | They rely on trial-and-error at your expense |
| SPC charts and Cpk data | The process stays stable over long runs | Quality depends on operator luck |
| Calibration records | Measurements are trustworthy | Inspection results mean nothing |
| Material certs and traceability | The right grade and temper went into your part | Silent material substitution risk |
| Incoming inspection procedure | Bad coil gets caught before the press | Defects travel downstream to you |
Match the Standard to Your Industry
Not every program needs IATF 16949 4. But if your stamped brackets go into automotive assemblies, a supplier without it will struggle with your customer's audit later. For general hardware and construction clips, ISO 9001 plus strong Cpk evidence on critical dimensions is usually enough. The point is fit, not maximum paperwork.
One more thing we check: whether inspection is built into the process or bolted on at the end. Strong suppliers run in-process checks at set intervals during production. Weak ones inspect a pile of finished parts and sort out the bad ones. Sorting is not quality control. It is damage control, and you pay for it in the piece price.
How Can I Evaluate a Supplier's Engineering and Co-Development Capabilities Before Signing a Contract?
There is a trade-off we weigh on every custom project: a supplier with strong engineering usually quotes higher tooling, but they also catch drawing problems before steel gets cut.
Evaluate engineering strength by testing the supplier's DFM feedback on your actual drawing, confirming in-house die design and CAD/CAM capability, reviewing their tooling build and maintenance approach, and checking references for past co-development projects with similar part geometry and tolerances.

The cheapest test costs you nothing: send your drawing and see what comes back. In our co-development work with U.S. engineering firms, we have noticed a clear pattern. Weak suppliers reply with only a price. Strong suppliers reply with questions — about tolerance stack-up on the bent flanges, about grain direction on tight-radius bends, about whether that elongated slot really needs ±0.05 mm or whether ±0.1 mm would work and cut tooling cost.
A Simple Pre-Contract Engineering Test
We recommend this sequence before awarding any tooling:
- Send the drawing with one deliberate ambiguity. A capable supplier will flag it. A passive one will not.
- Ask who designs the die. In-house die design 5 means faster changes and clear accountability. Fully outsourced die design with no internal engineering control is a warning sign.
- Request a DFM report. Look for specific comments on bend radii, hole-to-edge distance, springback compensation, and material choice.
- Ask about die maintenance. Strong suppliers show a preventive maintenance schedule and a die-life strategy, not just repairs after failure.
- Check a comparable case. Ask for an example of a past part with similar bends, gauge, and tolerances, plus its FAI report.
Why Early Engineering Input Saves the Program
On stamped brackets like Z-clips and multi-bend mounting parts, springback is the silent budget killer. A supplier who compensates for it in the die design gets the part right the first time. A supplier who does not will loop through tooling revisions — each one costing weeks. When we manage projects for purchasing managers, the "right first time" rate is the single strongest predictor of whether the program hits its launch date. Engineering capability is what drives that rate.
Which Red Flags Should I Watch for When Auditing a Stamping Parts Manufacturer's Production Process?
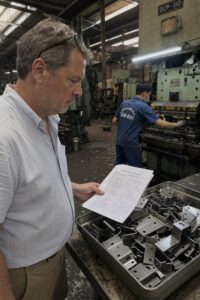
During one plant walk-through, I noticed a die stored on the floor under a leaking roof panel. The sales manager had just finished a polished presentation about quality. The die told the real story.
Watch for dies stored without protection or maintenance records, no in-process inspection at the press, missing material traceability, high operator turnover, single-die production with no backup, outsourced critical secondary operations, and quotes that hide tooling, inspection, or finishing costs inside the piece price.

An audit is where the marketing ends and the truth begins. Our Vietnam-based team walks plants regularly on behalf of overseas buyers, and the same warning signs repeat across factories of every size. The good news is that most red flags are visible within two hours if you know where to point your eyes.
The Red Flag Checklist We Use On-Site
| Area | Red Flag | Why It Hurts You |
|---|---|---|
| Die storage | Rust, floor storage, no maintenance log | Dimensional drift and surprise downtime mid-program |
| Press line | No first-piece or in-process checks | Defects run for hours before anyone notices |
| Material | Unlabeled coils, no cert matching | Wrong grade or gauge in your parts |
| Workforce | Mostly new operators, no training records | Inconsistent setups and scrap spikes |
| Capacity | Presses at full utilization, no redundancy | Your order slips when anything breaks |
| Secondary ops | Plating and welding fully outsourced, uncontrolled | Longer lead time and quality gaps you cannot see |
| Quoting | One lump-sum number, nothing itemized | Hidden costs surface after you commit |
Look at What They Measure, Not What They Say
Ask an operator — not the sales manager — how often critical dimensions get checked during a run. The answer tells you whether SPC is real or decorative. Then ask to see the scrap area. A clean, small, labeled scrap zone suggests controlled processes. A large unsorted pile suggests the opposite. Finally, check whether tooling for long-running parts has a spare or a refurbishment plan. Single-point tooling risk is one of the most overlooked failure modes in stamping programs, and it only reveals itself when the die cracks in month eight.
How Do I Assess a Supplier's On-Time Delivery Track Record and Payment Flexibility?
A purchasing manager we work with in the U.S. once told me his biggest fear was not price — it was the silent two-week slip that surfaces only after the ship date passes. We built our reporting cadence around that fear.
Assess delivery by requesting on-time delivery data for the past twelve months — 95 percent or better is a practical benchmark — verifying it with customer references and a trial order, and confirming payment flexibility such as open account or 60–90 day terms backed by the supplier's financial stability.

Delivery performance is a habit, not a promise. Any supplier will promise your lead time during the RFQ. The question is whether their system makes that promise come true, order after order. In our supply chain 6 work between Asia and the U.S., we have found the strongest predictor is not press speed. It is planning discipline: how the supplier schedules material, tooling, production slots, and outbound logistics as one connected plan.
How to Verify Delivery Claims
Use more than one source, because each has blind spots:
| Verification Method | What It Reveals | Limitation |
|---|---|---|
| Supplier's own OTD reports | Their internal tracking discipline | Can be selectively presented |
| Customer references | Real experience over a full program | References are hand-picked |
| Trial or sample order | Actual behavior under a real deadline | Small orders get special treatment |
| Communication response time | How fast problems will be flagged | Sales speed can differ from operations speed |
Run at least two of these before committing tooling. A trial order plus one reference call catches most weak performers.
Payment Terms Signal Financial Health
Payment flexibility matters for your cash flow, but it also works as a diagnostic. A supplier who can offer open account or 60–90 day terms is usually financially stable, because extending credit requires working capital 7. A supplier who demands full payment upfront on every order may be running on fumes — and financial distress often shows up as quality slippage or a sudden closure mid-project. We structure credit terms for our clients precisely because a program that ties up cash for months before parts arrive puts pressure on both sides. When you compare stamping parts suppliers, treat delivery data and payment terms as two views of the same thing: operational and financial health.
Conclusion
The strongest stamping parts suppliers prove repeatability with data, engineering depth, delivery discipline, and financial health. Score them on evidence, not quotes — the lowest-risk partner wins the program.
Footnotes
1. Background reference explaining CAD/CAM tools used in die design and engineering evaluation. ↩︎
2. Explains design-for-manufacturability principles referenced in the engineering evaluation checklist. ↩︎
3. Links to official ISO standard definition referenced as the baseline quality certification. ↩︎
4. ISO defines automotive quality management standards referenced for supplier certification benchmarks. ↩︎
5. Background reference on manufacturing dies relevant to in-house tooling capability discussion. ↩︎
6. Background concept link explaining supply chain planning discussed in delivery section. ↩︎
7. Defines working capital, key to understanding supplier payment terms and financial health. ↩︎
 English
 Español de México
 Deutsch
 Français
 Русский
 العربية
Leave a Comment
Your email address will not be published. Required fields are marked *